PET is one of the most moisture- and heat-sensitive packaging polymers on the market, so the extruder you choose directly determines intrinsic viscosity (IV), colour and final sheet toughness. A PET co-rotating twin-screw extruder gives processors a modular, controllable way to convey, melt, mix, degas and discharge PET — but only when the screw configuration matches the material. This guide explains how the technology works, what each screw element does, where degradation risk comes from and how TZ-machinery applies an 85 mm parallel co-rotating twin-screw system in industrial PET sheet extrusion lines.
What Is a PET Co-Rotating Twin-Screw Extruder?
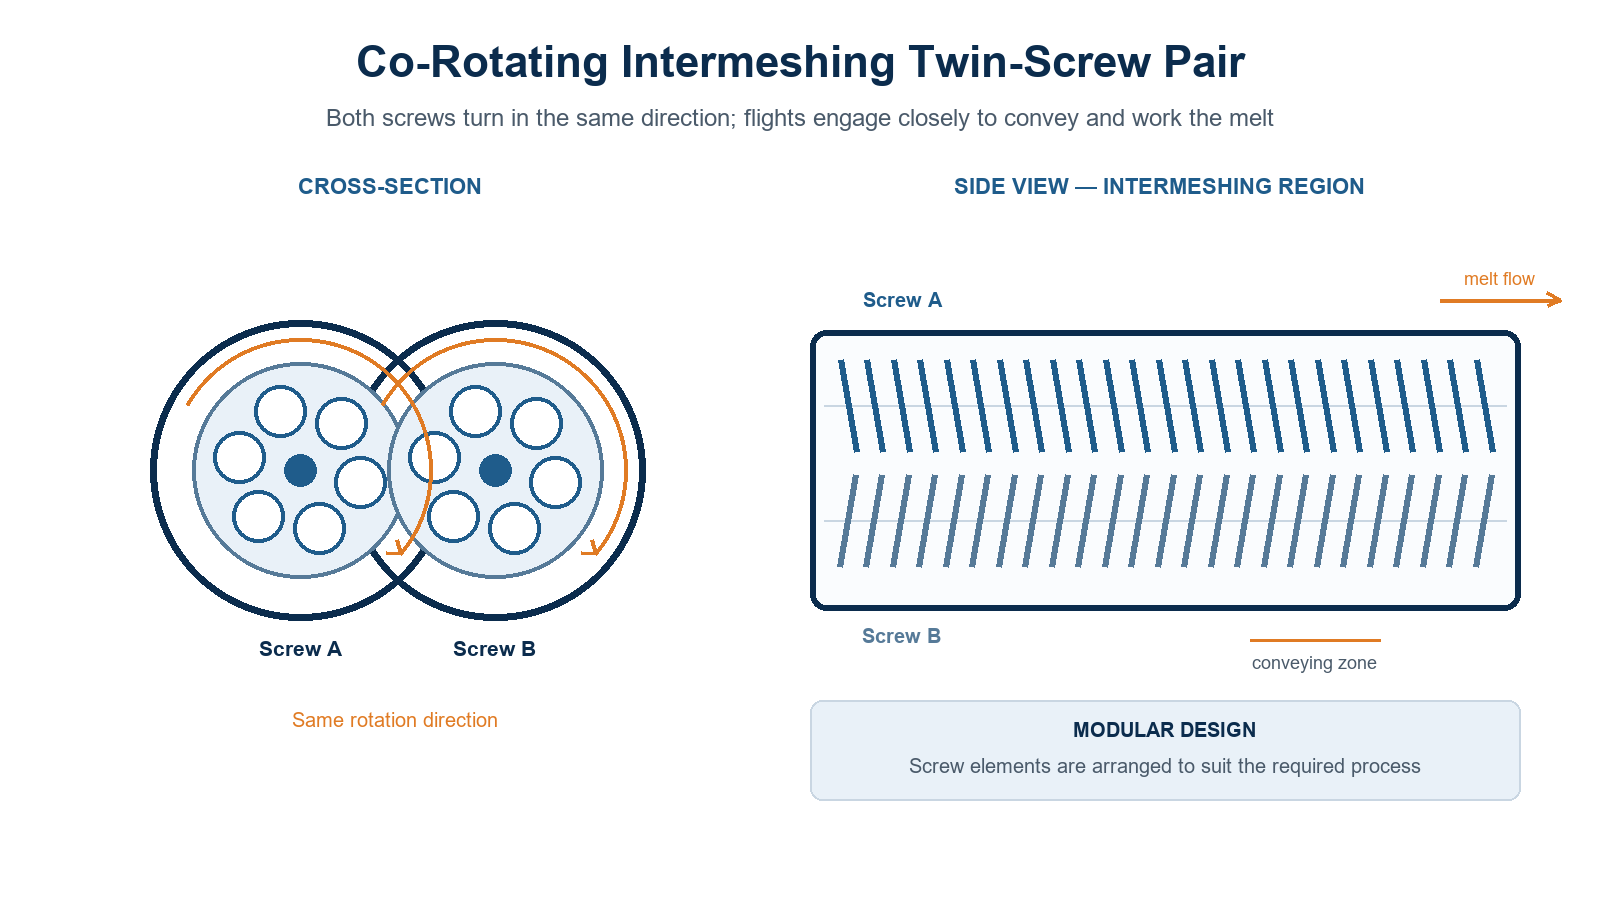
A twin-screw extruder uses two parallel screws inside one barrel. In a co-rotating design, both screws rotate in the same direction, and their flights intermesh closely to convey and work the melt. The screws are built from modular elements, so the process section can be arranged to suit the required application — devolatilization, compounding, or direct PET sheet extrusion.
Three characteristics define the design:
- Co-rotating: both screws turn in the same direction, self-wiping the flight flanks.
- Intermeshing: screw flights engage closely to convey and work the melt.
- Modular design: screw elements can be rearranged to suit the required process.
For a production-scale example, see the mesin ekstrusi lembaran PET sekrup kembar built around this 85 mm parallel co-rotating platform.
How PET Is Processed Inside the Extruder: Six Stages
Inside the barrel, PET passes through six functional stages:
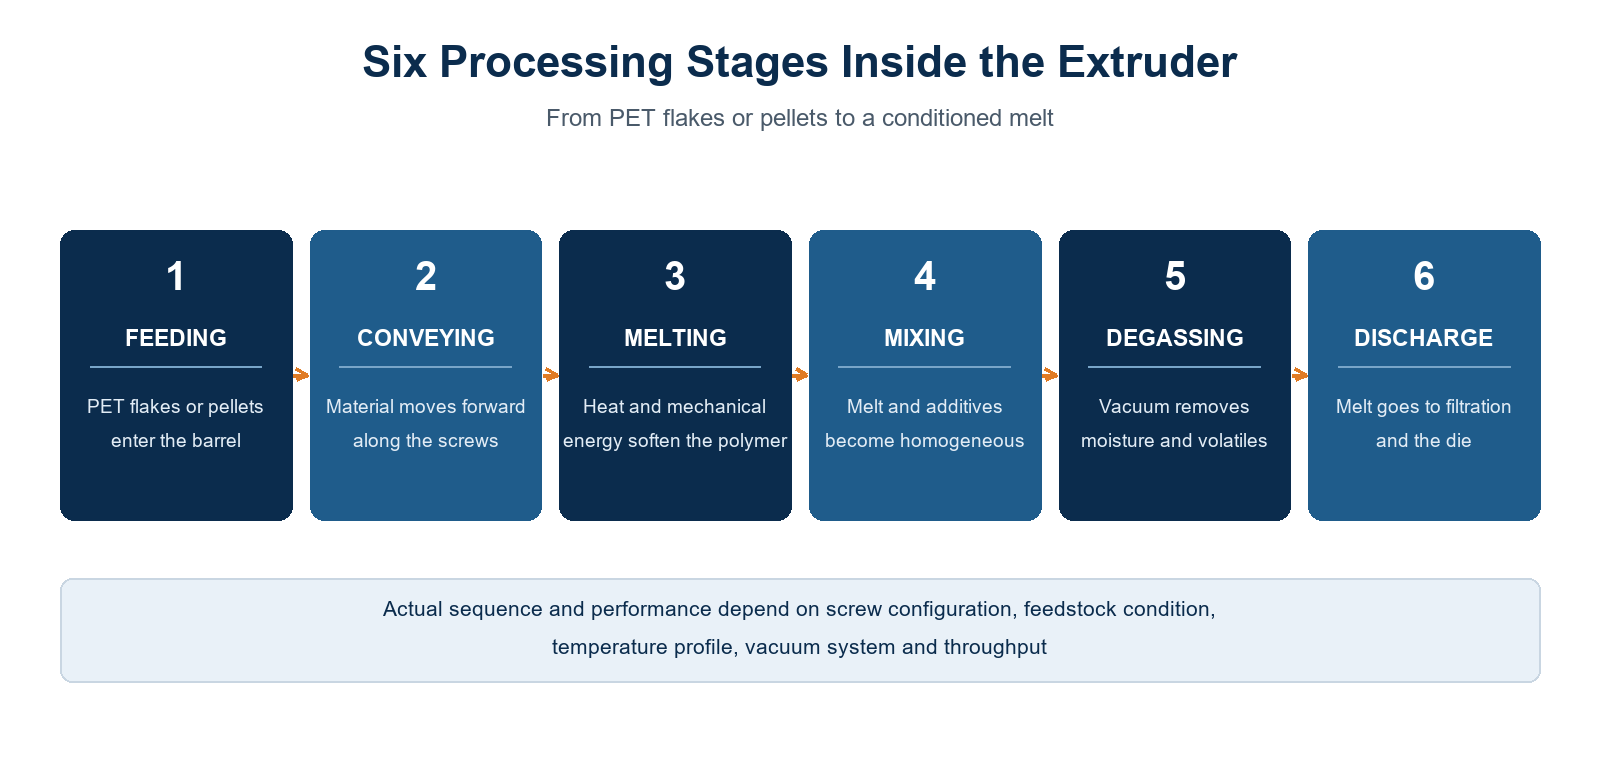
- Pemberian Makan — PET flakes or pellets enter the barrel.
- Conveying — material moves forward along the screws.
- Melting — heat and mechanical energy soften the polymer.
- Mixing — melt and additives become homogeneous.
- Degassing — vacuum removes moisture and volatile components.
- Discharge — the melt goes to filtration and the die.
The actual sequence and performance depend on screw configuration, feedstock condition, temperature profile, vacuum system and throughput.
The Four Screw Element Types and What They Do
A PET twin-screw process section is assembled from four basic element families:
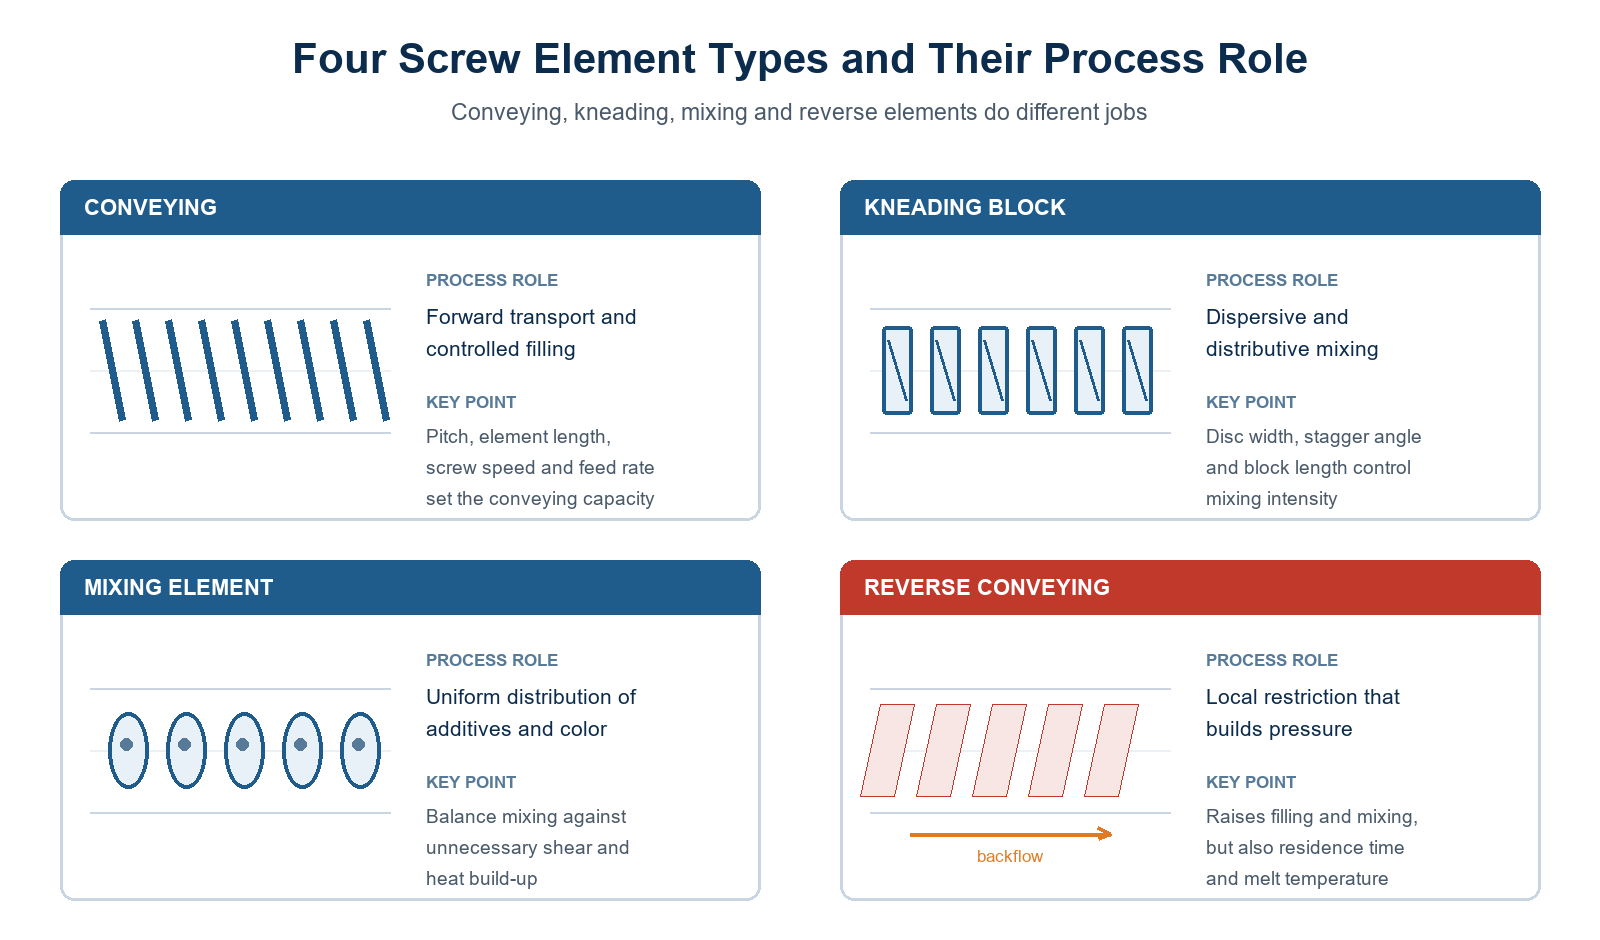
1. Conveying Elements — Forward Transport and Controlled Filling
Conveying elements move PET material forward along the barrel. They establish material transport, filling level and residence-time conditions. Pitch, element length, screw speed and feed rate all affect conveying capacity. Note that conveying elements provide transport rather than intensive mixing.
2. Kneading Blocks — Dispersive and Distributive Mixing
Kneading blocks split, recombine and deform the material as it passes through staggered discs. Disc width, stagger angle, block length, screw speed and throughput define the mixing action. PET caution: excessive mechanical energy can increase melt temperature and degradation risk — stronger mixing is not always better for PET.
3. Mixing Elements — Distribution and Formulation Uniformity
Mixing elements spread additives, colour masterbatch and different material components more evenly (distributive mixing) and break down agglomerates when sufficient stress is applied (dispersive mixing). Choose mixing intensity to achieve uniformity without unnecessary shear or heat.
4. Reverse Conveying Elements — Controlled Restriction
Reverse elements oppose forward conveying locally and create a pressure-building section. Correctly positioned, they can increase melt filling, mixing and degassing effectiveness. The risk: they may increase residence time, shear and melt temperature, so they must be used carefully. Reverse elements are process-control elements — not simply “stronger mixing” elements.
Vacuum Degassing: What It Can and Cannot Do
The vacuum port removes moisture and volatile components from the melt under suitable vacuum conditions. Effective degassing requires adequate melt surface renewal, sufficient vent area, proper vacuum capacity and stable operation.
Important limit: vacuum degassing does not guarantee that wet PET can be processed without drying. PET is moisture-sensitive at melt-processing temperatures, so feedstock moisture control remains critical. Vented single-screw lines such as the SWT-120D vented single screw PET sheet extrusion line follow the same principle — the vent system assists moisture and volatile removal, it does not replace correct drying.
How Screw Configuration Can Cause PET Degradation
Three mechanisms degrade PET during melt processing:
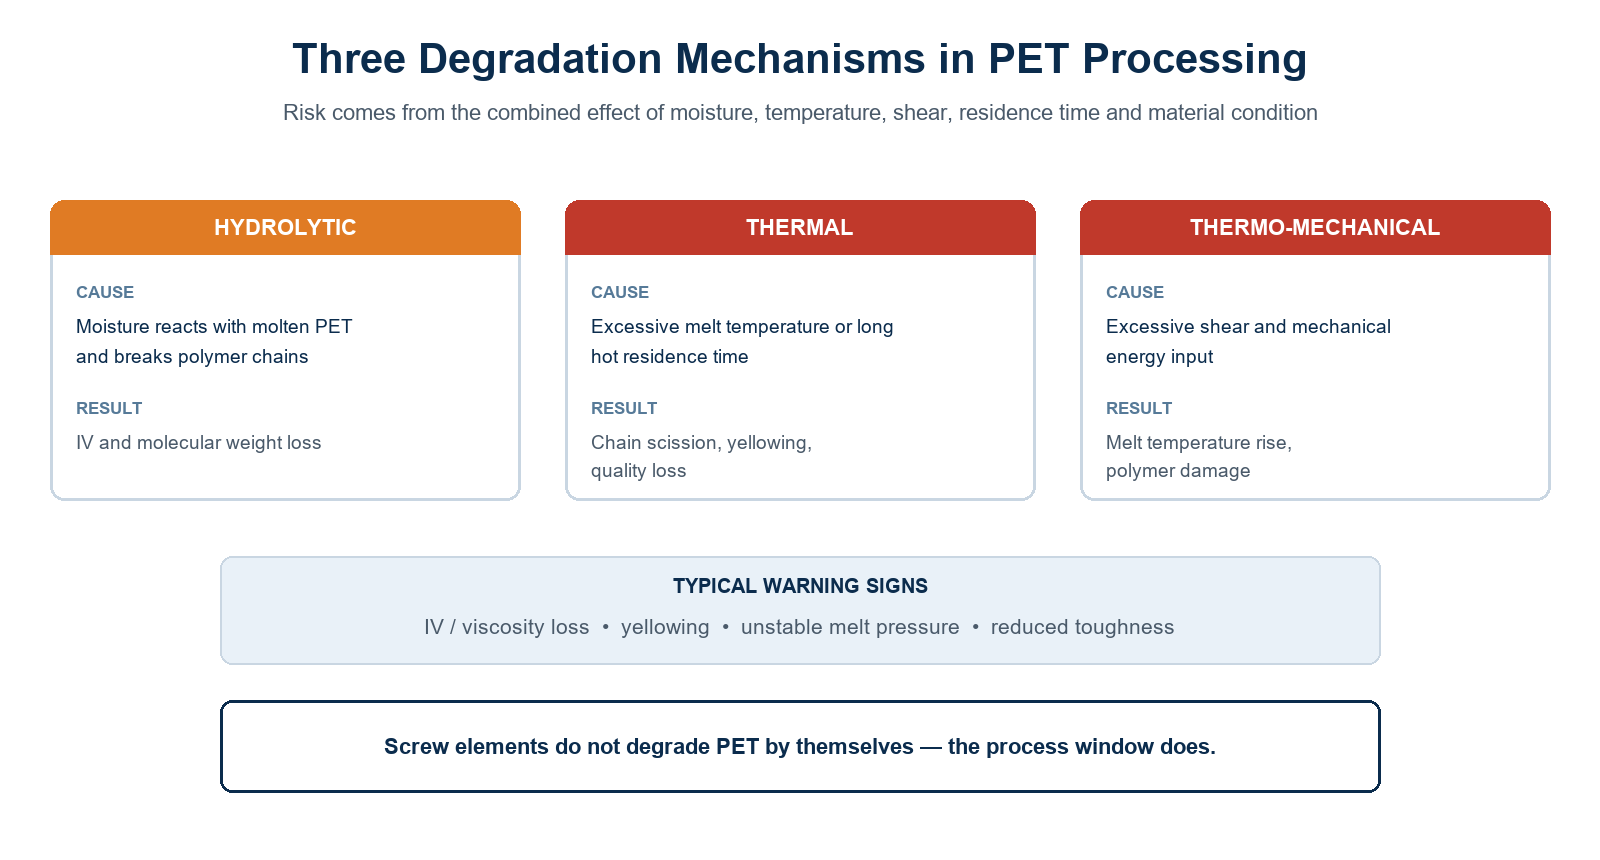
- Hydrolytic degradation — moisture reacts with molten PET and breaks polymer chains, reducing intrinsic viscosity (IV) and molecular weight.
- Thermal degradation — excessive melt temperature or long exposure at high temperature causes chain scission, discoloration and quality loss.
- Thermo-mechanical degradation — excessive shear and mechanical energy raise melt temperature and contribute to polymer damage.
Typical warning signs include IV or viscosity loss, yellowing, unstable melt pressure, and reduced toughness or forming performance. The screw elements do not automatically degrade PET — risk comes from the combined effects of moisture, temperature, shear, residence time and material condition.
Balancing Mixing Performance and PET Protection
Screw design is a balancing act. Too little mixing produces poor additive dispersion, uneven material composition and incomplete homogenization. Too much mechanical energy produces higher melt temperature, longer residence time in restrictive zones and greater degradation risk.
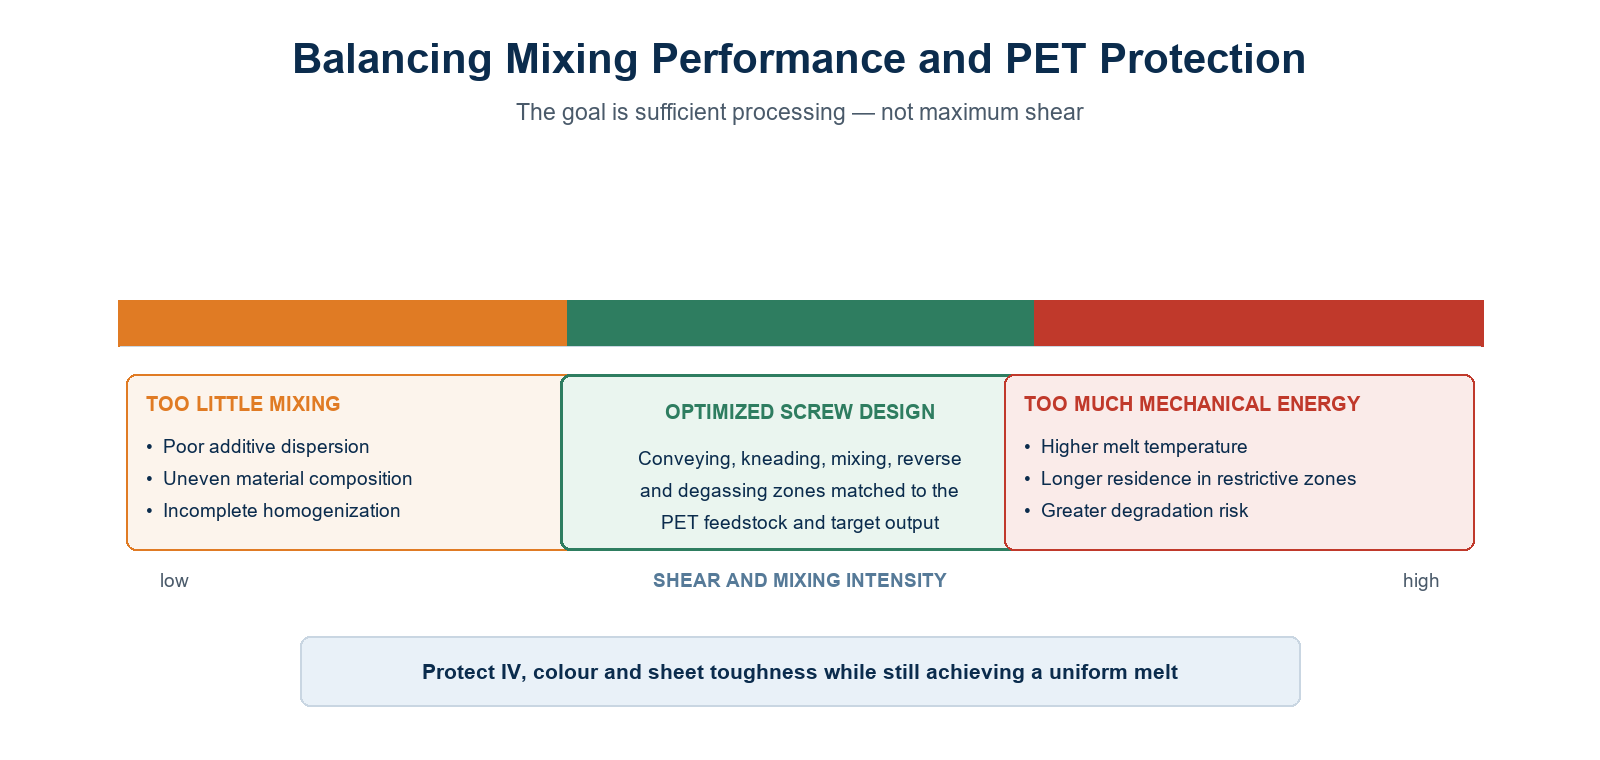
The optimized screw design matches conveying, kneading, mixing, reverse elements and degassing zones to the PET feedstock and target output — sufficient processing, not maximum shear.
Six Practical Measures to Reduce PET Degradation
| # | Measure | What to Do |
|---|---|---|
| 01 | Dry and control feedstock | Keep PET moisture within the raw-material and process specification. |
| 02 | Optimize melt temperature | Avoid unnecessary high temperatures and long hot residence times. |
| 03 | Select screw elements carefully | Use only the mixing intensity needed for the target formulation. |
| 04 | Avoid excessive restriction | Position reverse elements carefully and monitor pressure and temperature. |
| 05 | Stabilize throughput | Avoid prolonged idling with PET melt inside the barrel. |
| 06 | Monitor melt quality | Track IV where applicable, colour, pressure, output and sheet performance. |
Exact limits must be established from material supplier data, machine design and production trials.
Application: 85 mm Twin-Screw + 75 mm Single-Screw ABA Line
The technology reaches full value in a hybrid ABA sheet line, where the twin-screw and single-screw systems work together:
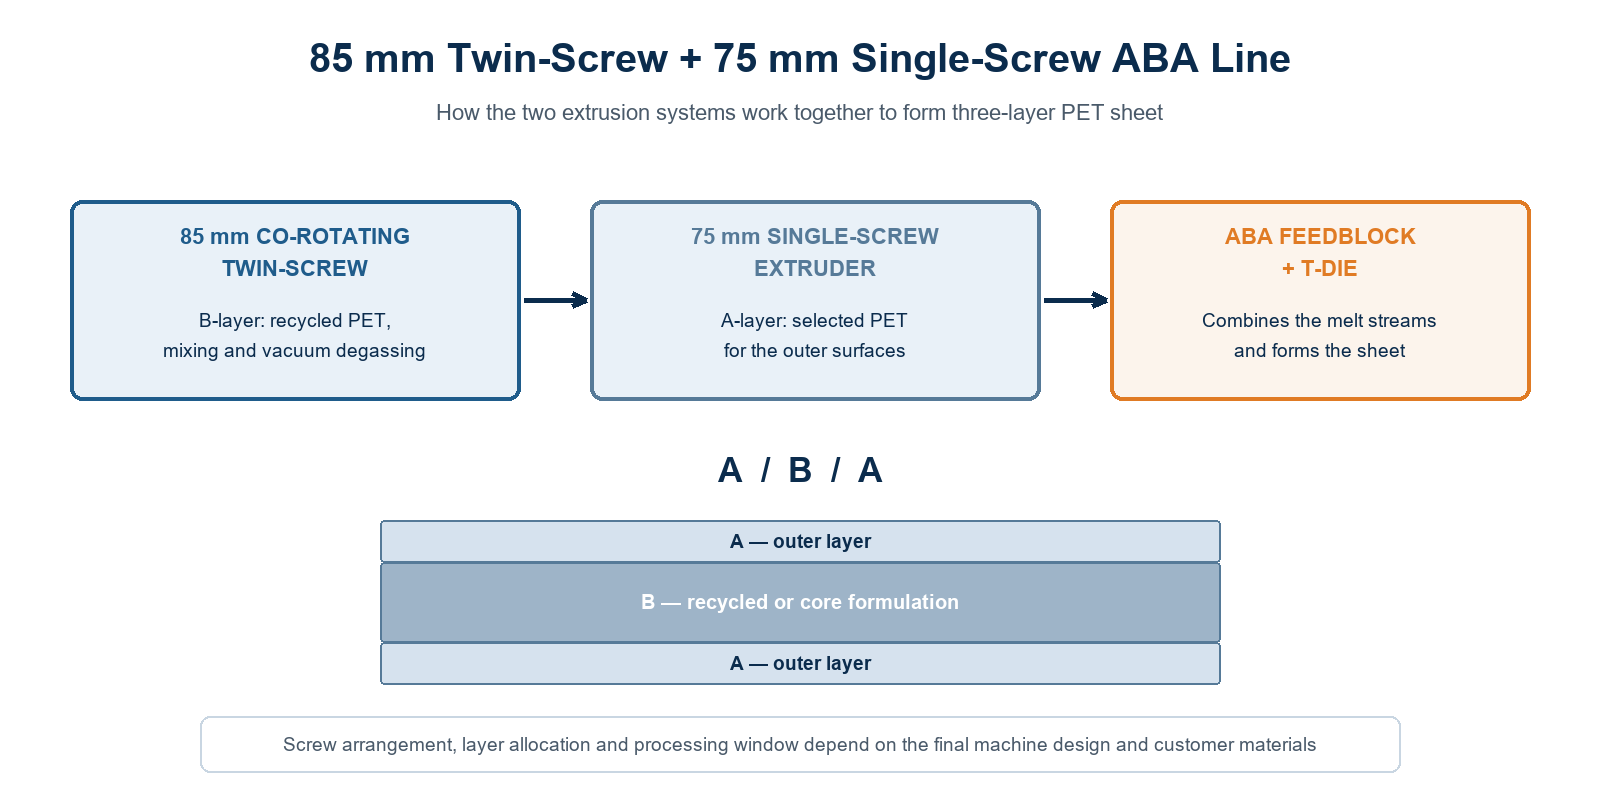
- 85 mm co-rotating twin-screw — B-layer processing: suitable recycled PET materials, mixing and vacuum degassing.
- 75 mm single-screw — A-layer processing: selected PET material for the outer surfaces (see the jalur produksi ekstrusi lembaran PET dengan sekrup tunggal).
- ABA feedblock + T-die — combines the melt streams and forms the three-layer PET sheet.
The result is an A/B/A structure: outer layers of selected virgin-quality PET around a core of recycled or alternative formulation. The full configuration is available in the Lini ekstrusi bersama lembaran tiga lapis ABA PET, which pairs both extrusion systems with a dedicated feedblock. Actual screw arrangement, layer allocation and processing window depend on the final machine design and the customer’s materials.
Poin-Poin Penting
Design the screw. Control the process. Protect PET quality. Effective conveying, balanced mixing, controlled degassing and a correctly limited use of restrictive elements together deliver lower degradation risk — and that is what separates a stable PET sheet operation from a constant IV-loss troubleshooting exercise. Every screw configuration should be verified against the specific feedstock, target output and sheet quality requirements before committing to a production window.