Recycled PET sheet extrusion often faces three major quality problems: yellowing, poor toughness, and insufficient gloss. These problems become more noticeable when using a high percentage of recycled PET flakes or regrind. For manufacturers producing PET thermoforming sheets, these defects can affect product appearance, forming performance, and final product quality.
1. Why Does Recycled PET Sheet Turn Yellow?
PET sheet may turn yellow due to thermal degradation, moisture-related hydrolysis, contaminated recycled materials, or excessive residence time at high temperatures. Proper raw material management and optimized extrusion conditions are essential.
For parallel twin screw PET sheet extrusion lines, appropriate screw configuration, temperature control, vacuum degassing, and effective melt filtration can help improve melt quality and reduce processing defects.
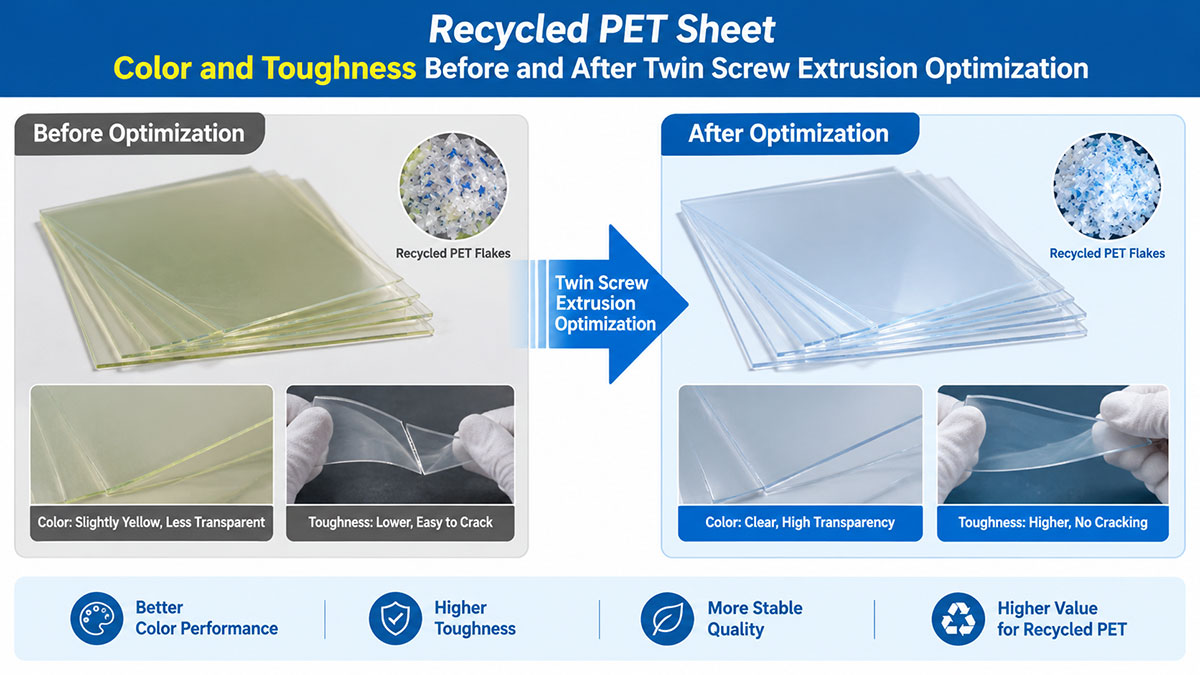
Recycled PET sheet color and toughness before and after twin screw extrusion optimization
2. How to Improve PET Sheet Toughness and Gloss
Poor toughness may result from PET molecular weight degradation, reduced intrinsic viscosity (IV), or inconsistent recycled material quality. Insufficient gloss may be related to contamination, melt uniformity, die conditions, or cooling roller settings.
In addition to optimizing the extrusion process, manufacturers can consider the following masterbatch formulations as starting points for production trials.
| Masterbatch Type | Recommended Addition per 1,000 kg of PET |
|---|---|
| Anti-yellowing masterbatch | 300-600 g |
| Toughening / anti-cracking masterbatch | 6-8 kg |
| Whitening masterbatch | 1.5 kg |
| Gloss-enhancing masterbatch | 1.5 kg |
These dosages are reference formulations and should be validated according to the masterbatch supplier’s specifications, recycled PET quality, and required sheet properties. Whitening and gloss-enhancing masterbatches can improve appearance, while toughening additives may help improve impact performance. Actual results depend on additive compatibility and processing conditions.
3. How Parallel Twin Screw Extrusion Improves Recycled PET Sheet Quality
A properly designed parallel twin screw PET sheet extrusion line can provide effective mixing, degassing, and processing of suitable recycled PET materials. Combined with appropriate filtration, temperature control, and accurate additive dosing, it can help manufacturers improve sheet color consistency, toughness, and surface appearance.
The optimal equipment configuration and processing parameters depend on recycled material composition, target output, sheet thickness, and final application. Maintaining stable raw material quality and controlling PET degradation are also essential for consistent production results.
الأسئلة الشائعة
لماذا تتحول ألواح البولي إيثيلين تيريفثالات (PET) المعاد تدويرها إلى اللون الأصفر؟
هناك أربعة أسباب رئيسية: التحلل الحراري، والتحلل المائي المرتبط بالرطوبة، والمواد المعاد تدويرها الملوثة، ووقت البقاء المفرط عند درجة حرارة انصهار عالية. ويُعد الاصفرار تغيرًا كيميائيًّا في سلسلة البوليمر، لذا يُفضل التحكم فيه في المراحل الأولية من خلال إدارة المواد الخام، والتحكم في درجة الحرارة، وإزالة الغازات بالفراغ، وترشيح المادة المنصهرة.
هل يمكن عكس عملية الاصفرار بعد إنتاج الورقة؟
لا. فالاصفرار يعكس تغيرًا جزيئيًّا في مادة البولي إيثيلين تيريفثالات (PET) نفسها، لذا لا يمكن إزالته بالتلميع أو الغسل لاحقًا. والحل العملي هو الوقاية: الحفاظ على جفاف ونظافة الرقائق، وتقليل مدة البقاء، وإضافة مادة أساسية مضادة للاصفرار بجرعة معتمدة.
لماذا تفقد ألواح البولي إيثيلين تيريفثالات (PET) المعاد تدويرها صلابتها ومقاومتها للصدمات؟
عادةً ما يتبع فقدان الصلابة انخفاضًا في الوزن الجزيئي واللزوجة الذاتية (IV). تصل الرقائق المعاد تدويرها بقيم متفاوتة للزوجة الذاتية وتاريخ متفاوت من التعرض للحرارة، لذا قد تحتوي المادة المنصهرة على أجزاء متدهورة تتشقق عند التعرض للصدمات. وتساهم جودة الرقائق المتسقة والمعالجة الحرارية اللطيفة في الحفاظ على الزوجة الذاتية.
How much anti-yellowing masterbatch is used per ton of PET?
A common starting point is 300-600 g per 1,000 kg of PET. The exact level depends on the masterbatch supplier’s specification, the color of the incoming recycled flakes, and the target sheet appearance, so it should be confirmed in production trials.
How much toughening masterbatch is added to recycled PET sheet?
A reference dosage is 6-8 kg per 1,000 kg of PET, which is roughly ten times the anti-yellowing addition. Impact performance depends on additive compatibility with the base resin and on processing conditions, so validate the level on your own line before scaling up.
Does a twin screw line need pre-drying for recycled PET flakes?
Vacuum degassing and multi-vent design remove moisture and volatiles during extrusion, which reduces the crystallization and pre-drying burden that a خط بثق صفيحة PET أحادية اللولب normally requires. Extremely wet or heavily contaminated flakes may still need upstream conditioning.
What causes poor gloss on recycled PET sheet?
Insufficient gloss usually traces to contamination, poor melt uniformity, die conditions, or cooling roller settings. Stable melt pressure, clean filtration, and controlled cooling all have a direct effect on surface finish.
Can an ABA co-extrusion structure hide recycled PET discoloration?
Yes. An ABA PET three-layer co-extrusion line places virgin outer skins over a recycled core, so slight core discoloration is much less visible on the finished product. It is a practical option when recycled content is high but surface appearance must stay premium.
How can sheet producers keep recycled material quality consistent?
Close the loop in-house. A كسارة خردة الصفائح الحافة على الإنترنت returns skeletal waste directly to the extruder, so the regrind stream stays clean, dry, and traceable instead of accumulating unknown contamination.